
What testing is for
A bearing can look perfect and still be wrong in ways the eye cannot see: a raceway slightly out of round, clearance outside its group, a soft ring, a noisy ball. Testing exists to catch these before shipment. The desk does not own a test laboratory; it works with the inspection rooms of partner plants and, where a project requires it, with independent third-party labs. Instruments are described here by type and parameter class, because what matters is whether the instrument class suits the tolerance grade being checked. Equipment suitability is part of the plant screening, and the checks that use it are set in the inspection plan.
Methods and instruments
| Property | Method and instrument type | What it tells you |
|---|---|---|
| Boundary dimensions | Bore and outside gauges, micrometers, width gauges | Conformance to ISO 15 sizes and the ISO 492 tolerance class ordered |
| Radial clearance | Clearance gauge with a defined measuring load | Whether the bearing falls in the ordered group, such as CN or C3 |
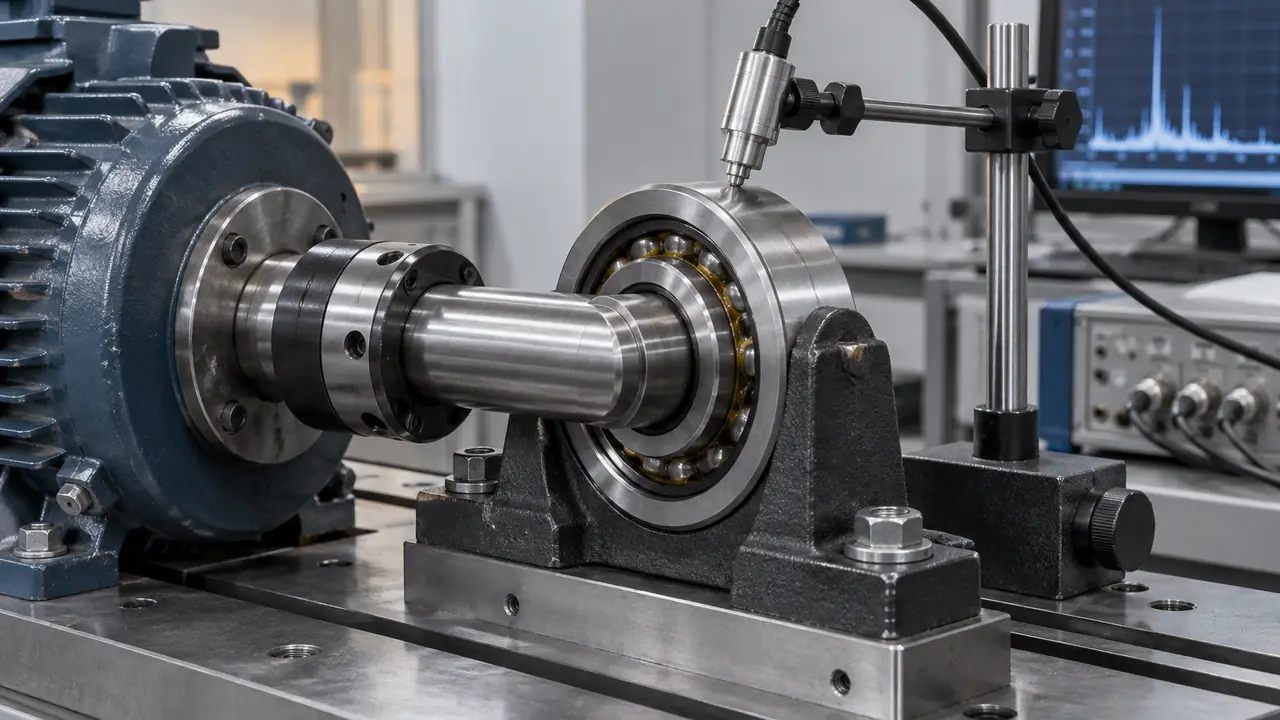
| Vibration and noise | Vibration tester with spindle rig, bandpass analysis, sound room for noise-critical lots | Smoothness of raceways and balls against the agreed vibration grade |
| Roundness and profile | Roundness and profile measuring equipment | Form of raceways and rings, source of many noise problems |
| Hardness | Rockwell hardness tester on sampled parts | Heat-treatment result on rings and rolling elements |
| Surface roughness | Contact stylus roughness tester | Finish of raceways and mating surfaces |
| Cleanliness | Visual check, rinse test where required | Absence of residue and particles |
| Rotation | Manual rotation, torque rig where specified | Smoothness and absence of catching |
| Seals and grease | Visual and opened-sample check | Seal fit and lip, grease type and appearance |
| Endurance | Endurance rig at plant or third-party lab | Behaviour under defined load, speed and time |
Vibration and noise
Vibration is the most informative single test on a ball bearing. The bearing is spun on a rig at a set speed and axial load, and the vibration signal is read in frequency bands. Grades such as Z1, Z2 and Z3 or V1, V2 and V3, associated with company practice and the GB/T 24610 system, are agreed per order; values are not published here because they depend on the series and the rig. Low-noise programs for motors and appliances are the typical users, as described on motors and appliances.
Clearance, form and hardness
Radial internal clearance is checked on the clearance gauge with a stated measuring load, since the reading depends on it. Clearance decides how the bearing behaves after the fit and under heat, which is why the C3 group is common for motors (C3 clearance explained). Roundness and profile equipment reveals form errors that a micrometer misses. Hardness is sampled on rings and rolling elements because the test marks the part. The report states the sample size used.
Endurance testing
Endurance testing runs bearings under a stated load, speed and temperature for a defined time, and observes failures or changes. It is slow and costly, so it is not run on every lot. It is used at program start, when a material or supplier changes, or when a customer needs life evidence beyond the ISO 281 rating life calculation. It is performed at a partner plant that has the rig or at an independent lab, per project, and the test conditions are written down. This site does not publish life or rating figures; those come from the supplier datasheet, derived under ISO 281 and ISO 76.
What goes into a lot report
- Lot identification: designation with suffixes, lot number, quantity and production period.
- Sampling basis: plan reference, sample sizes, acceptance criteria.
- Results: dimensions, clearance, vibration, hardness, roughness, cleanliness, rotation and seal checks, as agreed.
- Visual and marking check against the golden sample.
- Packing and anti-rust confirmation, with carton counts and labels.
- Material certificate reference for steel, and RoHS or REACH declaration where requested (see certifications).
Third-party inspection
If your quality system requires independent verification, the desk can arrange an inspector to attend the final inspection or a lab to run selected tests, either on a program basis or on a particular lot. The scope, such as dimensions, vibration, hardness and packing checks, is agreed before the visit, and the third-party report is issued directly to you alongside the plant report. Costs and timing are confirmed in writing. To discuss what your program needs, use the quote form.