
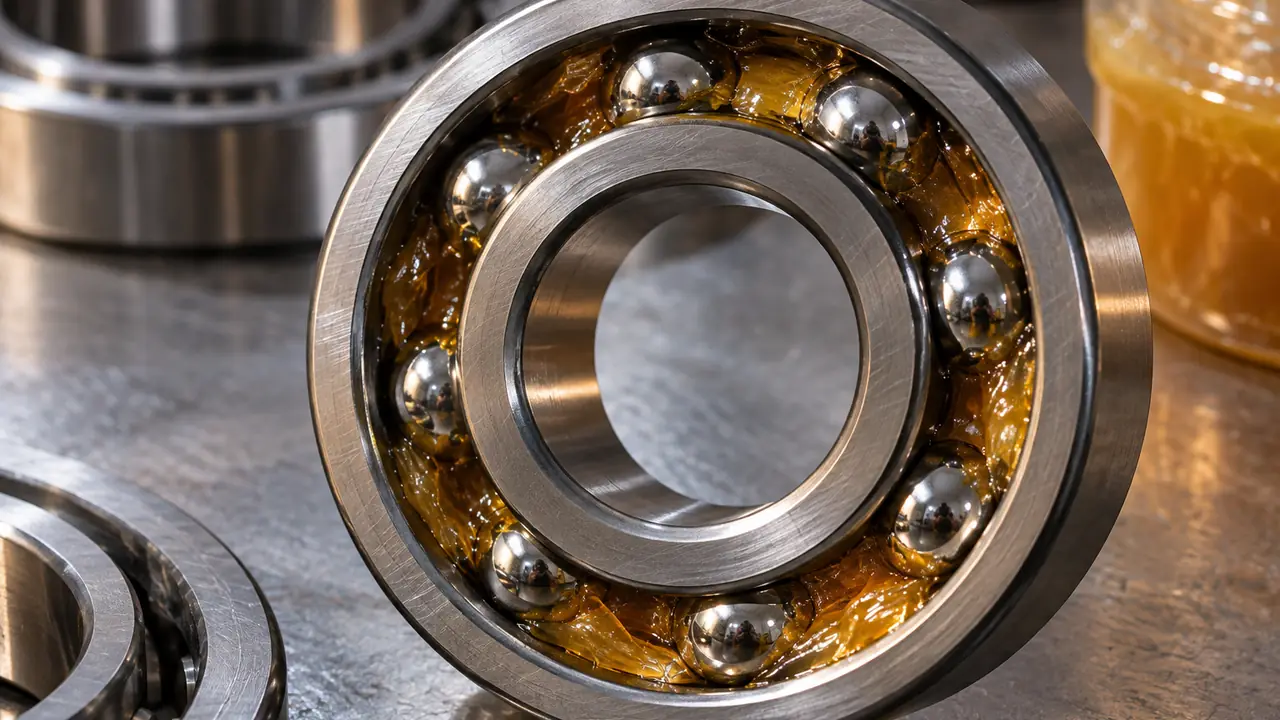
The main rule: push on the ring that is tight
A bearing is usually fitted tight on one ring and looser on the other. The ring with the interference fit, normally the inner ring on a rotating shaft, is the one you push. The mounting force must pass through that ring only, never through the rolling elements. If you push the outer ring to seat an inner-ring fit, the force travels through the balls or rollers and dents the raceways. The marks are called Brinell dents and they cause noise and early fatigue, often with no visible sign from outside.
When both rings are tight, as in some gearbox or wheel assemblies, use a mounting sleeve or disc that loads both faces at the same time. When the bearing sits on a tapered seat or an adapter sleeve, the fit is set by the axial drive-up distance, not by pushing on the face.
Preparation before anything touches the shaft
- Keep the bearing in its packing until the last moment. The anti-rust coating is protective; do not wash it off from a new, sealed or greased bearing. For open bearings that are to be oil lubricated, wipe or flush only as the supplier instructs.
- Clean the work area, shaft and housing. Dirt in the seat or on the bearing is the main source of early failure. Remove burrs, paint and rust from the seat with fine abrasive cloth, and wipe with a clean lint-free cloth.
- Check the dimensions. Measure shaft and housing seats with a micrometre or bore gauge and compare with the recommended fit, such as k5 or m6 on the shaft and H7 in the housing. Also check shoulder squareness and fillet radius so the ring seats flat.
- Confirm the bearing designation, clearance group and seals against the drawing before mounting.
- Prepare the lubricant, the sleeve or tool, and a plan for orientation of seals and markings.
Mounting methods compared
| Method | Suited to | Main caution |
|---|---|---|
| Mechanical or hydraulic press with sleeve | Small to medium bearings with light interference | Align the press; use a sleeve that touches only the tight ring |
| Hand tools with a fitting-tool kit | Small bearings, occasional repairs | Use even taps on a sleeve, never direct hammer blows |
| Induction heater | Medium to large inner rings, repeat work | Heat evenly, avoid overheating, demagnetise if required |
| Oil bath or oven heating | When no induction heater is available | Control temperature; hot oil and surfaces are a burn risk |
| Cooling the shaft or bearing | Small parts, light interference | Condensation risk; dry and coat with protective oil |
| Oil injection and hydraulic nut | Tapered seats and large spherical or tapered roller bearings | Follow the drive-up values from the supplier |
Heating a bearing safely
Heating expands the inner ring so that it slides onto the shaft. A widely quoted guideline is to heat to about 80 to 90 C above the shaft temperature for ordinary interference fits, and never beyond the temperature limit of the bearing, commonly published around 120 C for standard bearings. Check the datasheet for the limit of your bearing, the grease and the seals. Do not use an open flame or a torch; local overheating softens the steel and ruins the heat treatment.
Sealed or shielded bearings with grease should not be heated in an oil bath; use an induction heater at a lower temperature and follow the supplier limit. Wear heat-resistant gloves, use lifting tools for heavy parts, and keep the area clear of bystanders. Once the bearing is on the shaft, push it against the shoulder and hold it there until it cools so it does not shrink away from the shoulder.
Tools and habits to avoid
- Do not hammer on the bearing, cage or seal with a hammer or punch. Hardened steel chips can fly off and injure people, and the ring can be damaged.
- Do not use a pipe wrench, pliers or chisel to push the ring.
- Do not press through the rolling elements.
- Do not mount a bearing that has been dropped or shows signs of rust, dents or discolouration.
- Do not use compressed air to spin a clean bearing; it can run dry at high speed and drive dirt into the raceway.
- Do not reuse a bearing that was removed by a method that loaded the rolling elements.
Wear safety glasses, gloves suited to the job, and use the tool that matches the bearing size. Lifting heavy bearings by hand risks injury; use slings or lifting aids.
Fitting housed units and taper-bore bearings
Housed units such as pillow blocks and flange units are usually secured with set screws or an eccentric collar. Slide the unit onto a clean, burr-free shaft, align the housing on its frame before final tightening, and then lock the inner ring. If you lock the ring first and bolt the housing down afterwards, a skewed frame forces the bearing out of alignment. Use shims where the mounting surface is uneven.
Bearings with a tapered bore sit on an adapter or withdrawal sleeve, or directly on a tapered shaft. The fit is set by how far the bearing is driven up the taper, so you measure the clearance before and after mounting with a feeler gauge, or follow the axial drive-up value from the supplier. Do not tighten the nut to a guessed torque. Excess drive-up removes internal clearance and the bearing overheats quickly; too little leaves the ring free to creep on the sleeve.
Checking the result
After mounting, turn the shaft by hand. It should rotate smoothly with no catching, grinding or uneven drag. Check that the bearing is square against the shoulder with a feeler gauge, and that the locking device (nut, lock washer, circlip or set screw) is correctly fitted. For housed units, confirm the grub screws or eccentric locking collar are tightened to the supplier torque. On first start, listen and measure temperature for the first hour or two. A temperature rise that settles at a steady level is normal; a continuing rise points to excessive preload, too much grease, or a misaligned housing. Troubleshooting temperature issues is covered in the bearing overheating guide.
Order the right parts with the bearing
Installation goes more smoothly when the right accessories are on hand: adapter sleeves, lock nuts and washers, circlips, and mounting sleeves of the correct size. Include them in your quote request together with the bearing designation and fits. Ask for the supplier's mounting recommendations, and treat the figures in this note as general guidance and not a replacement for them.